Key Takeaway
Most Steel Wire Armoured (SWA) cable failures on job sites are not standard material degradation. They stem from improper specification for aggressive soils, physical abuse during installation, or hidden factory cuts in conductor cross-sections.
Having manufactured and exported medium and low-voltage armoured cables since 1980, Huanghe Cable has analyzed hundreds of field failure cases across mining, solar, and industrial projects in Africa, Southeast Asia, and Central Asia. Below are the 10 most costly SWA cable failure modes, their root physics, and the exact specification rules to prevent them.
Failure 1: Steel Wire Armour Corrosion in Acidic & Coastal Soils
What Happens
The galvanised steel wire armour (SWA) layer rusts away within 12–36 months of direct burial. The outer PVC sheath may look intact, but underneath, the steel wires lose structural integrity and snap. Moisture then penetrates the inner sheath, directly attacking the metallic screen and copper conductors, leading to catastrophic phase-to-earth faults.
Primary Regions
Coastal Southeast Asia (Indonesia, Philippines, Vietnam), West Africa (Nigeria, Ghana), and tropical mining districts with acidic laterite soils.
Root Cause
- Sub-standard Galvanisation: BS 5467 and IEC 60502-1 mandate galvanised steel wire, but low-cost suppliers often use electro-galvanised wire with a zinc layer as thin as 15–30 g/m². Acidic soils quickly consume this thin layer.
- Aggressive Soil Chemistry: Laterite soils across tropical regions frequently have a pH of 4.0–5.5. High moisture combined with ambient temperatures above 30°C accelerates steel corrosion to over 0.1 mm per year.
- Stray DC Currents: Mining haulage systems and DC traction lines cause stray currents to flow through buried steel armour, inducing localized electrochemical pitting.
Prevention & Specification
- Specify Heavy Hot-Dip Galvanisation (HDG): Require a minimum zinc coating weight of 180–290 g/m² (per BS EN 10244-2 Class A), rather than standard commercially galvanized wire.
- Upgrade the Outer Sheath: For soils with pH < 5.0 or high salinity, specify an outer sheath of MDPE or HDPE instead of standard PVC. Polyethylene forms an impermeable barrier against soil moisture.
- Pre-shipment Verification: Request factory test reports for zinc coating mass per ISO 1460 / BS EN 10244 prior to dispatch.
Failure 2: Sheath Degradation and Insulation Treeing from UV Storage
What Happens
Cable drums sit in open site yards for months before trenching. Direct sunlight degrades the black PVC outer sheath, causing micro-cracking and plasticizer loss. After installation and energization, moisture ingress through these micro-cracks creates electrical treeing in the XLPE insulation, resulting in sudden breakdown under load.
[Sunlight/UV Exposure] ➔ [PVC Plasticizer Loss] ➔ [Micro-Cracking] ➔ [Moisture Ingress] ➔ [XLPE Insulation Treeing]
Primary Regions
Middle East, Sahel region (Mali, Niger, Chad), and high-altitude tropical solar farms (Kenya, Mexico).
Root Cause
Standard PVC compounds without carbon black stabilization cannot withstand continuous UV indices exceeding 11. Dark cable sheath surface temperatures in direct tropical sun can exceed 75°C, accelerating thermal aging and embrittlement.
Prevention & Specification
- Specify UV-stabilized, Carbon Black-loaded (minimum 2.5% concentration) Polyethylene (PE) or High-Density PVC for outer sheathing.
- Require reflective, waterproof tarpaulins over stored cable drums on site.
- Ensure cable ends are sealed with heavy-duty heat-shrink end caps—not standard electrical tape—to prevent moisture breathing during ambient temperature cycles.
Failure 3: Termite and Rodent Attack on Buried Sheathing
What Happens
Subterranean termites or rodents chew through the outer sheath. Termites release acidic secretions (formic acid, pH ~2.5) that dissolve PVC, rapidly corroding the underlying SWA layer. Rodents gnaw on sheaths due to the presence of bio-based plasticizers, exposing live cores.
Primary Regions
Southeast Asia (Malaysia, Thailand, Indonesia), Sub-Saharan Africa, and agricultural infrastructure projects.
Root Cause
Standard PVC offers no chemical or mechanical resistance against Coptotermes termite species, which exert mandible pressures sufficient to puncture soft polymers.
Prevention & Specification
- Chemical Protection: Specify Anti-Termite/Anti-Rodent PVC or PE sheath, incorporating non-hazardous termiticides (e.g., Cypermethrin additives at 0.5–1.0%).
- Physical Protection: For severe termite zones, specify a Polyamide (Nylon PA12) jacket extruded over the outer sheath. Nylon is too hard for termites to bite and immune to formic acid.
- Note: Major utilities like Malaysia’s TNB strictly require anti-termite sheathing for buried networks.
Failure 4: Severe Overheating from Single-Core SWA in AC Circuits (Eddy Current Losses)
What Happens
Single-core SWA cables installed in an AC system run extremely hot—often melting the outer sheath and insulation within hours of full-load operation—even when the copper conductor is sized correctly.
Root Cause
Basic Electromagnetic Physics Error: Steel is a ferromagnetic material. When alternating current (AC) passes through a single conductor inside a magnetic steel wire cage, it induces circulating magnetic flux and eddy currents in the SWA layer. The steel armour effectively acts as an induction heater.
Prevention & Specification
- Rule: NEVER use Steel Wire Armour (SWA) for single-core AC cables.
- Correct Specification: Specify Aluminum Wire Armour (AWA) for single-core AC circuits. Aluminum is non-magnetic, eliminating eddy current heating losses.
- Note: SWA is acceptable for single-core DC circuits (e.g., solar string main runs) as static DC fields do not induce eddy currents.
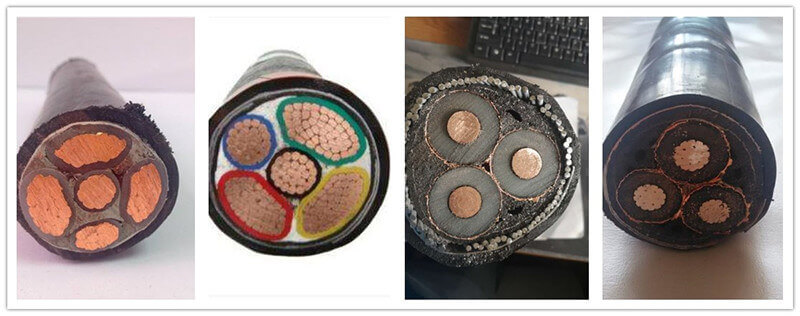
Failure 5: Sheath Splitting and Core Distortion from Oversimplified Bending
What Happens
During cable pulling around trench corners or duct banks, the outer sheath splits open on the outer radius, and internal cores crush against each other on the inner radius.
Root Cause
Exceeding the Minimum Bending Radius (MBR) during installation.
| Cable Configuration |
Standard Minimum Bending Radius (per IEC 60502-1) |
Example (50mm Outer Diameter Cable) |
| Multi-core SWA Cable |
12 × Overall Diameter (D) |
600 mm Minimum Radius |
| Single-core AWA Cable |
15 × Overall Diameter (D) |
755 mm Minimum Radius |
Civil installation crews frequently pull heavy cables around sharp 90° masonry corners without corner rollers or radius restrictors, over-stretching the PVC sheath past its elongation limit.
Prevention & Specification
- Mandate the use of ground rollers and corner guide sheaves along the entire trench path.
- Clearly stamp the Minimum Bending Radius on the outer sheath and drum labels before shipping from the factory.
Failure 6: Capillary Moisture Ingress via Unsealed Cut Ends
What Happens
Water enters cut cable ends during ocean transit, heavy rainfall in open trenches, or prolonged storage. Capillary action draws water meters deep into the conductor stranding. When energized, moisture causes immediate insulation tracking or long-term conductor corrosion.
Root Cause
Leaving cut cable ends exposed or wrapped with basic PVC tape, which unravels under heat and humidity.
Prevention & Specification
- Mandate factory-applied, heavy-duty adhesive heat-shrink end caps on both ends of every cable drum prior to container loading.
- Require longitudinal water-blocking tape (swelling tape) under the sheath for cables installed in flooded trenches or duct banks.
Failure 7: Under-sized Conductors & Sub-standard Copper (Supply Chain Fraud)
What Happens
A cable specified as 4 × 95 mm² experiences excessive voltage drop, overheats under nominal design current, and trips breakers. Thermal imaging reveals the conductor is running at 105°C under 70% rated load.
Root Cause
Supplier fraud. Common cost-cutting tactics by unethical manufacturers include:
- Undersizing: Supplying 82 mm² or 85 mm² of copper while stamping “95 mm²” on the sheath.
- Impurities: Using low-grade, recycled scrap copper with high electrical resistivity instead of Electrolytic Tough Pitch (ETP) copper (99.9% purity).
Prevention & Specification
- Conduct DC Conductor Resistance Testing (IEC 60228): Do not rely on physical diameter measurements alone. Measure electrical resistance in ohms/km at 20°C. High-purity copper must meet strict resistance ceilings (e.g., max 0.193 Ω/km for 95 mm² Class 2 conductor at 20°C).
- Pre-shipment Inspection: Engage independent third-party inspectors (SGS, Bureau Veritas, or Intertek) to conduct resistance tests directly on factory drums before loading.
Failure 8: Standard Mismatch and Regional Compliance Rejection
What Happens
Cables arrive at the destination port or job site and fail utility inspection or customs clearance because construction details do not match local utility codes.
Root Cause
Ordering cables built to generic domestic standards rather than the specific destination country standard.
Standard Alignment Matrix:
- Anglophone East/Southern Africa: BS 5467 / BS 7870 / SANS 1507
- Francophone West/Central Africa: NFC 33-226 / NFC 32-321
- International & Middle East: IEC 60502-1 / IEC 60502-2
For instance, French-standard NFC 33-226 requires specific outer sheath markings, core color coding, and semi-conductive screen dimensions that differ significantly from British Standard BS 5467.
Prevention & Specification
- Always state the exact reference standard, system voltage (U₀/U), and core color code on purchase orders.
- Partner with export-experienced manufacturers who provide standard-compliant type test reports from accredited bodies (such as KEMA, TUV, or CNAS).
Failure 9: Improvised Armour Earthing and Touch Potential Hazards
What Happens
During an insulation earth fault, the SWA layer becomes energized. Because the armour is improperly grounded, protective switchgear fails to trip, resulting in high touch voltages on equipment frames and serious electrical hazards.
Root Cause
Installers stripping the SWA layer and simply twisting a small earth wire around the steel wires rather than using proper rated cable glands.
Prevention & Specification
- Always use certified brass cable glands (BW for indoor dry use, CW for outdoor weatherproof environments) designed to clamp 360° around the steel wire armour to maintain low-impedance earth continuity.
- For multi-core cables, ground the SWA at both ends. For single-core AWA cables, utilize single-point earthing with sheath voltage limiters (SVL) to eliminate circulating currents while maintaining safety.
Failure 10: Theft and Vandalism on Unsecured Infrastructure Sites
What Happens
Stored drums or laid cable runs are cut open and stolen for scrap copper value, bringing civil construction to a halt.
Root Cause
High scrap copper prices make exposed heavy-power cables prime targets in remote or low-income project areas.
Prevention & Specification
- Aluminum Conductor Alternatives: For long-distance feeder lines, specify Aluminum Conductor SWA/AWA Cables. Aluminum delivers equal conductivity at a larger cross-section while carrying negligible scrap value, eliminating theft incentives.
- Physical Burial Depth: Bury copper runs to a minimum depth of 900 mm with concrete protective cover tiles laid directly above the cable line.
SWA vs. STA Cable: Quick Selection Guide
When specifying armoured cables for direct burial, choosing between Steel Wire Armour (SWA) and Steel Tape Armour (STA) is critical:
| Feature |
SWA (Steel Wire Armour) |
STA (Steel Tape Armour) |
| Armour Structure |
Round galvanised steel wires |
Double galvanised steel tape wraps |
| Tensile Strength |
Very High (Handles pulling tension) |
Low (Compressive strength only) |
| Best Application |
Direct burial, rocky soil, vertical drops, underground ducts |
Flat trenches, static indoor/duct installations |
| Single-Core AC Use |
Must use AWA (Aluminum Wire) |
Not suitable for single-core AC |

Why Global EPCs Partner with Huanghe Cable
Established in 1980 as a state-owned manufacturer and restructured for global trade, Huanghe Cable manufactures medium and low-voltage power cables, control cables, rubber cables, and overhead conductors designed for harsh environments.
- Full Compliance Manufacturing: Production lines configured to IEC 60502-1, BS 5467, NFC 33-226, and SANS 1507.
- Engineered Protection: Custom extrusion options including 200g/m² HDG steel wire, anti-termite PA12 jackets, and UV-stabilized HDPE outer sheaths.
- 100% Quality Assurance: Factory-equipped for full DC conductor resistance testing, insulation spark testing, and galvanisation weight verification.
- Inspection Ready: We welcome third-party pre-shipment inspections (SGS, Bureau Veritas, Intertek) on all export orders.
Need Engineering Support or Factory-Direct Pricing?
Whether you are preparing a bill of quantities (BOQ) for a mining project in Africa, a solar farm in Southeast Asia, or an industrial park in Central Asia, our technical engineering team is ready to assist.
📩 Send us your Cable Schedule or Project Inquiry today. We provide technical compliance sheets, full type-test reports, and competitive FOB/CIF quotations within 12 hours.
Related Guides
PVC Power Cable Procurement Guide 2026
The Ultimate MV/LV Power Cable Procurement Guide: Quality, Compliance, and Risk Mitigation for Buyers
XLPE Power Cables for Southeast Asia: Why Choose a Manufacturer Since 1980?
Need Cost-Effective XLPE Power Cables? Contact Huanghe Cable, a Trusted Chinese Factory, Directly for a Quote